0

Welcome!!

preview

So I enjoyed r/Machining on Reddit, but Reddit kinda dead, so I decided to make a new community! Thanks for looking feel free to post. -Edit I also want to say thanks for interacting and helping me out with identifying tools and stuff, I hope to learn a lot from you all, and I hope you can learn something from me as well Cheers!!!

So I enjoyed r/Machining on Reddit, but Reddit kinda dead, so I decided to make a new community! Thanks for looking feel free to post. -Edit I also want to say thanks for interacting and helping me out with identifying tools and stuff, I hope to learn a lot from you all, and I hope you can learn something from me as well Cheers!!!

0

Update to my previous post regarding taking a job in CAD/CAM generative AI

preview

cross-posted from: lemmy.sdf.org/post/61853810

Here’s the original post: lemmy.sdf.org/post/61773916

I spent my remaining $1,000 to get a lawyer regarding this. It was worth doing, I think because this could have set me up for a long time in a $600/mo apartment and I’ve been homeless recently (this story is really fucking complicated and I’m not willing to get into it for any reason). The legal advice boiled down to essentially my lawyer contacting theirs and reviewing a potential contract. The verdict? “It doesn’t hold water and there’s likely no real money there. They are trying to exploit you.” - which was something I thought may be happening anyway. If it smells like shit… etc.

So, if you receive this an offer like this - run. I don’t want to list the company name for potential doxxing reasons because their hiring pool is very limited. Down side is that I’m very broke now. It was worth a shot, I guess.

I’m also now in a really bad position because I just drained my bank account for a lawyer in the hopes of potentially being set up for years and the odd chance of kicking off a revolution via potentially hundreds of thousands of lost US jobs.

I’m going to be homeless again in a few weeks, but at least this time I have a car. If mods are ok with it, I’d like to link my webcomic (and therein is a support link, though it’s kind of buried).

Fuck AI.
cross-posted from: lemmy.sdf.org/post/61853810

Here’s the original post: lemmy.sdf.org/post/61773916

I spent my remaining $1,000 to get a lawyer regarding this. It was worth doing, I think because this could have set me up for a long time in a $600/mo apartment and I’ve been homeless recently (this story is really fucking complicated and I’m not willing to get into it for any reason). The legal advice boiled down to essentially my lawyer contacting theirs and reviewing a potential contract. The verdict? “It doesn’t hold water and there’s likely no real money there. They are trying to exploit you.” - which was something I thought may be happening anyway. If it smells like shit… etc.

So, if you receive this an offer like this - run. I don’t want to list the company name for potential doxxing reasons because their hiring pool is very limited. Down side is that I’m very broke now. It was worth a shot, I guess.

I’m also now in a really bad position because I just drained my bank account for a lawyer in the hopes of potentially being set up for years and the odd chance of kicking off a revolution via potentially hundreds of thousands of lost US jobs.

I’m going to be homeless again in a few weeks, but at least this time I have a car. If mods are ok with it, I’d like to link my webcomic (and therein is a support link, though it’s kind of buried).

Fuck AI.

0

Ethics of of an AI based contract?

preview

I’ve gotten several job listings from Indeed that require CAM programming and access to a CNC. I have both. They’re offering ~$135 per hour. The catch is that you use your usual work flow, make a part that your normally would and then remotely upload the results to this company so that they can train their AI to program CNC machines. I’m very against generative AI, but wow is that a lot of money for a 1 year contract. It took me 16 years to get good. Another 4 to make my own shop. But around 300k a year? It makes it hard. I’d love to know what other machinists think about this kind of thing.
I’ve gotten several job listings from Indeed that require CAM programming and access to a CNC. I have both. They’re offering ~$135 per hour. The catch is that you use your usual work flow, make a part that your normally would and then remotely upload the results to this company so that they can train their AI to program CNC machines. I’m very against generative AI, but wow is that a lot of money for a 1 year contract. It took me 16 years to get good. Another 4 to make my own shop. But around 300k a year? It makes it hard. I’d love to know what other machinists think about this kind of thing.

0

Both of the fans broke on my 6 year old laptop simultaneously, Good thing I just happened to have large scraps of aluminum to heat sink until the fans arrive.

preview

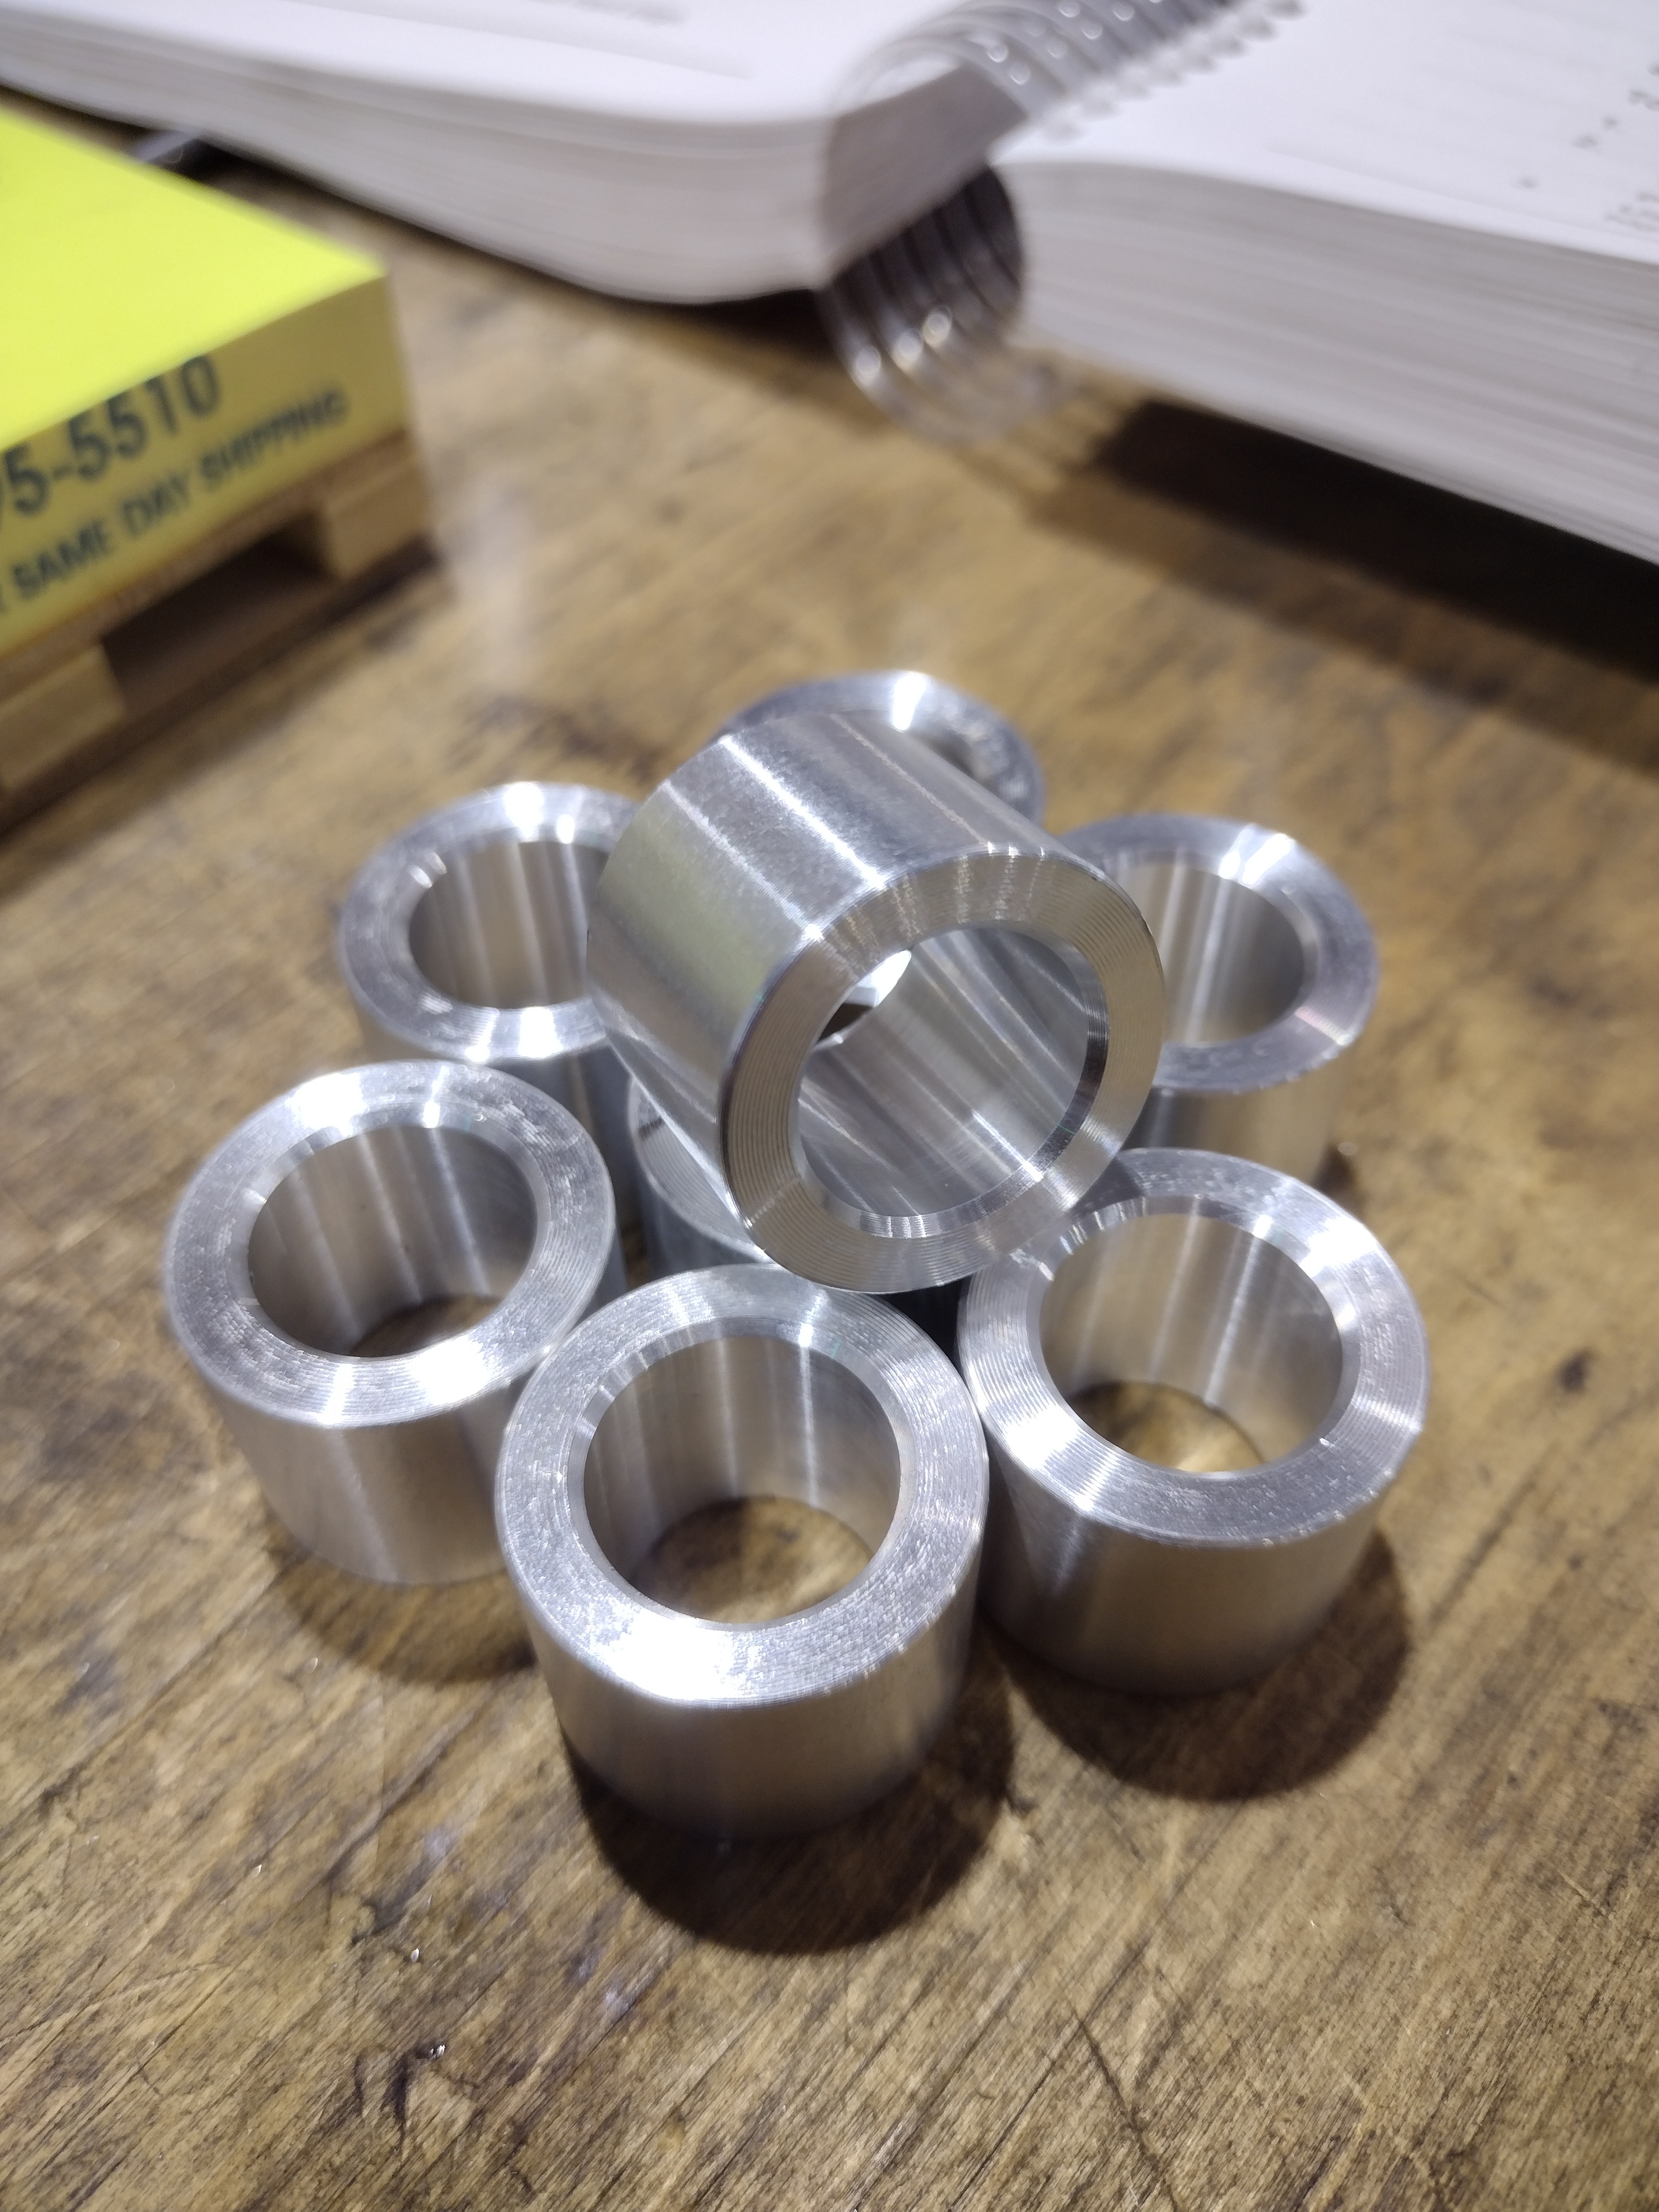
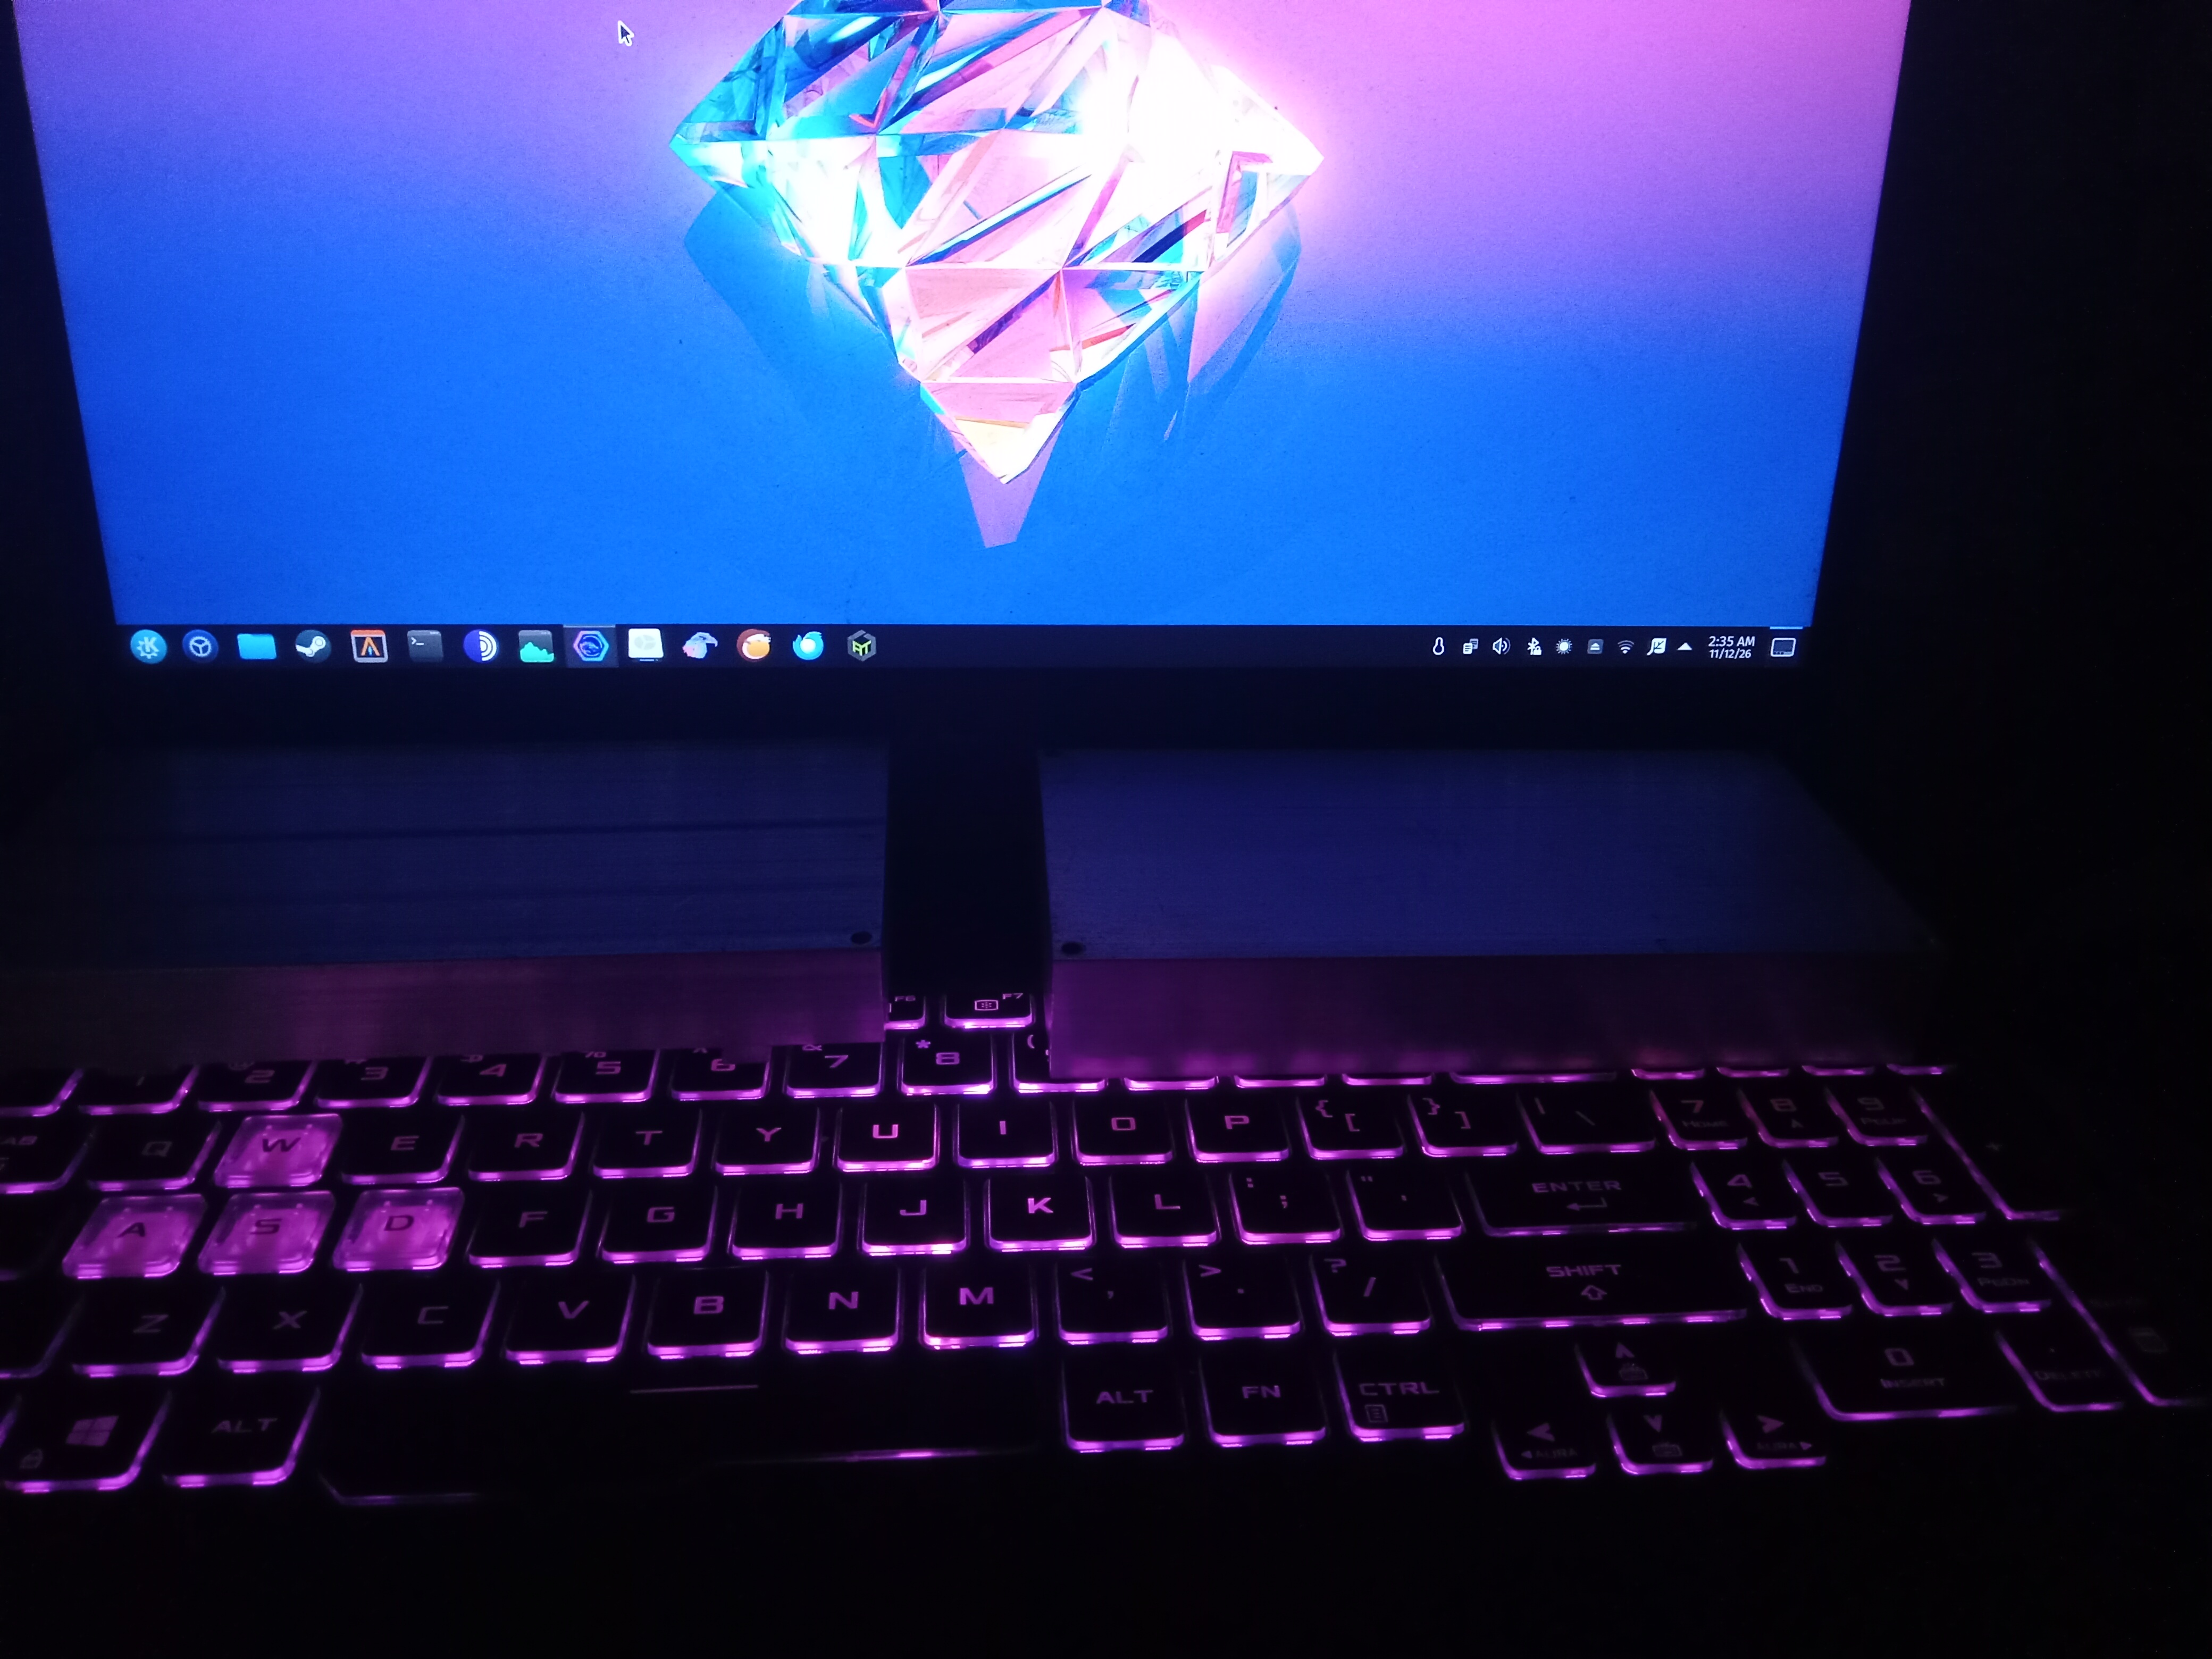
There are another 4 blocks under the laptop to further dissipate heat. Off camera, there is a large box fan and a ceiling fan keeping it from thermal death. Sometimes, keeping scrap can help immensely.

I just need one day of web browsing at 80 C to keep it alive (I hope).

ETA: the acutual pic

There are another 4 blocks under the laptop to further dissipate heat. Off camera, there is a large box fan and a ceiling fan keeping it from thermal death. Sometimes, keeping scrap can help immensely.

I just need one day of web browsing at 80 C to keep it alive (I hope).

ETA: the acutual pic

0

Left hand boring head?

preview

Working on boring out this hole to 7.5", need to insert the tool holder on the end like this on my boring head. Last time I did this part, I just ran the tool in reverse and took light cuts. This time the entire head unscrews any time I touch material. Do I need a LH insert holder to run the tool out like this now?

Working on boring out this hole to 7.5", need to insert the tool holder on the end like this on my boring head. Last time I did this part, I just ran the tool in reverse and took light cuts. This time the entire head unscrews any time I touch material. Do I need a LH insert holder to run the tool out like this now?

0

Help identifying spindle nose type?

preview

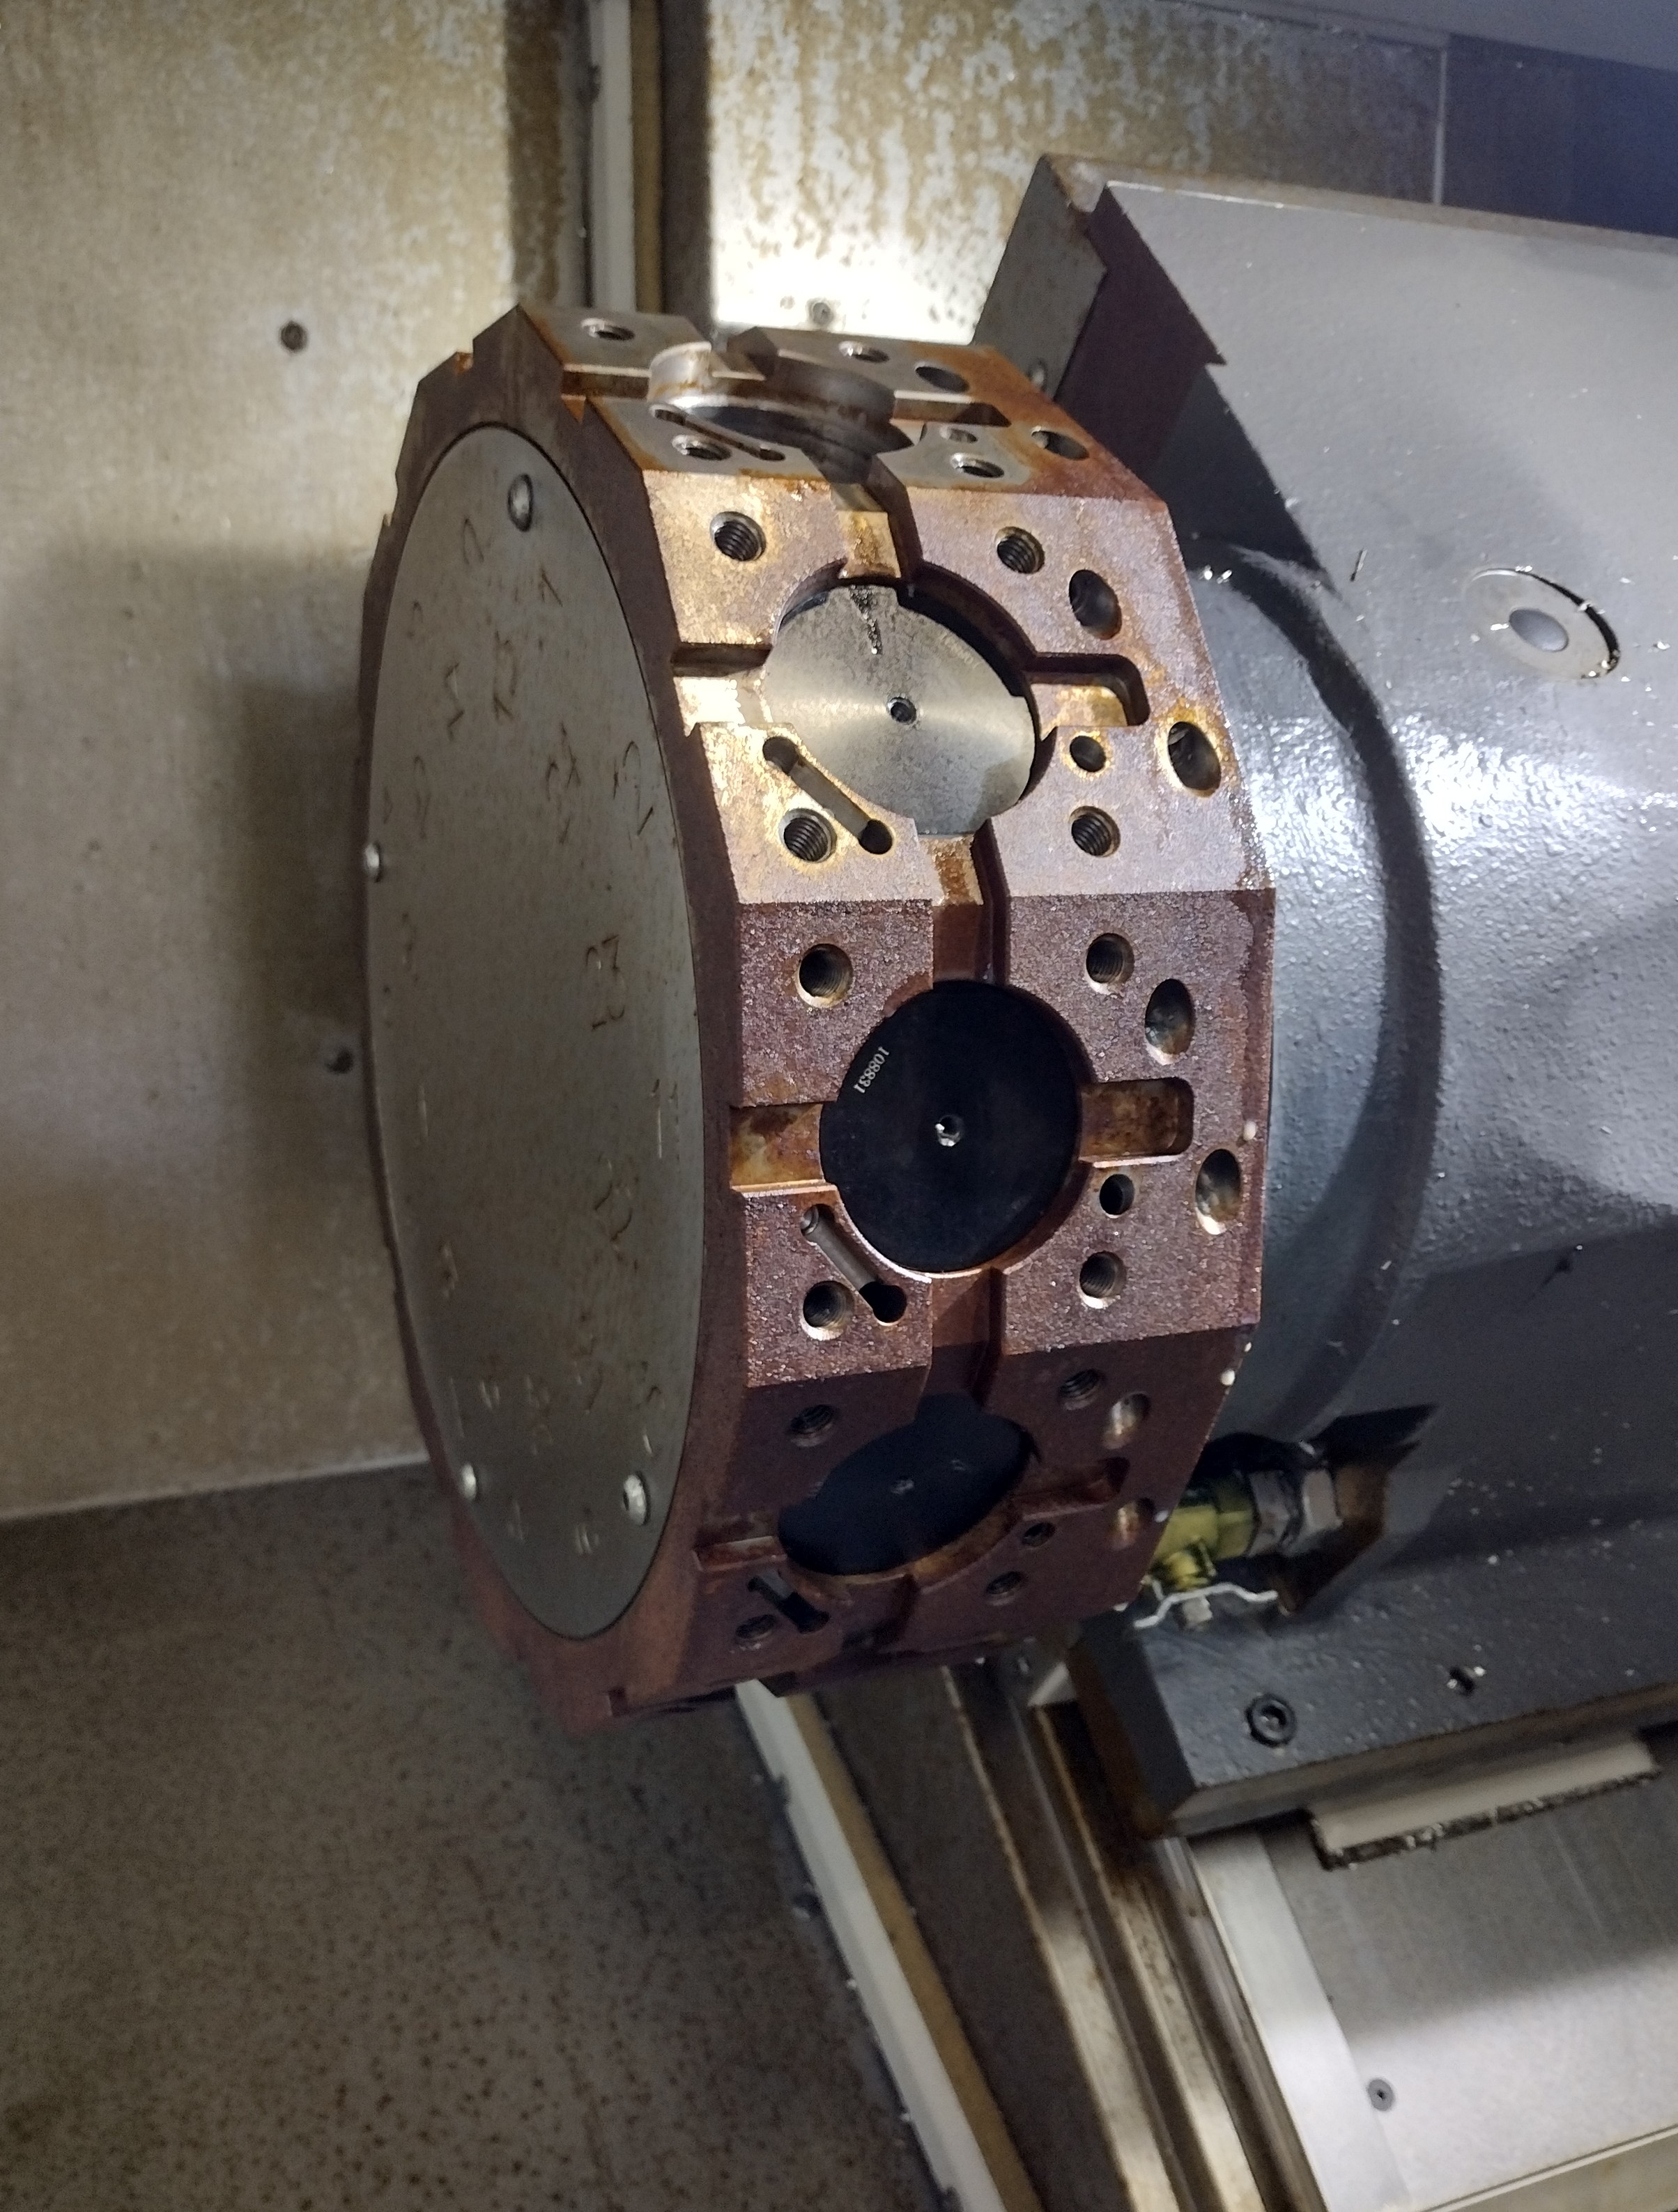
Got this old Szim lathe I’m working with at a new shop and in trying to identify what style of spindle nose this is. It looks like a typical short taper except the threaded holes are on the chuck/adapter plate instead of on the spindle nose. Haven’t seen this style before and I’d like to have a name that will let me look for more adapter plates/chucks designed for this spindle nose.

Looks like a type A2-8 short taper except the holes on the spindle nose aren’t tapped. It’s got this weird slotted bolt hole pattern on the back that rotates into place to secure the bolt heads while the bolts actually thread into the back of the chuck or adapter plate.

Thanks in advance.

Got this old Szim lathe I’m working with at a new shop and in trying to identify what style of spindle nose this is. It looks like a typical short taper except the threaded holes are on the chuck/adapter plate instead of on the spindle nose. Haven’t seen this style before and I’d like to have a name that will let me look for more adapter plates/chucks designed for this spindle nose.

Looks like a type A2-8 short taper except the holes on the spindle nose aren’t tapped. It’s got this weird slotted bolt hole pattern on the back that rotates into place to secure the bolt heads while the bolts actually thread into the back of the chuck or adapter plate.

Thanks in advance.

0

German investigators raid machine tool manufacturer Spinner over suspicions of equipment supplies to Russia

The Insider in English German investigators raid machine tool manufacturer Spinner over suspicions of equipment supplies to Russia theins.press
preview

cross-posted from: lemmy.sdf.org/post/39759212

crosspostato da: lemmy.sdf.org/post/39759210

Archived

German prosecutors and customs investigators have raided the premises of a machine tool manufacturer near Munich. The company is suspected of supplying more than 20 high-precision machines worth approximately €5.5 million to Russia in violation of European Union sanctions. Three company employees have been formally charged. Raids were also carried out in Baden-Württemberg and Bulgaria.

According to an investigation by Süddeutsche Zeitung, the company in question is Spinner, based in Sauerlach, a town just outside Munich. Spinner manufactures machine tools at various sites, including near Stuttgart, as well as in Bulgaria and Turkey.

In connection with the investigation, a Spinner machine subject to export restrictions was confiscated in mid-February 2025. Export documents indicated that the machine was supposed to leave Germany in August 2023, traveling through Poland and Belarus on its way to Uzbekistan. Investigators suspect the machine was in fact delivered to a Russian company affiliated with the manufacturer. There is also evidence of additional deliveries through Turkey and China.

The Munich prosecutor’s office cited a detailed report that aired in late April on the TV channel Arte, which traced the export of a Spinner machine to Russia via third countries — allegedly with the use of falsified documents. In the Arte report, one of the company’s three managing directors, Nikolaus Spinner, denied the allegations, claiming the machine had been sold to an Uzbek agricultural equipment manufacturer. However, a manager at the Uzbek company told reporters by phone that no such purchase had taken place.

[…]

cross-posted from: lemmy.sdf.org/post/39759212

crosspostato da: lemmy.sdf.org/post/39759210

Archived

German prosecutors and customs investigators have raided the premises of a machine tool manufacturer near Munich. The company is suspected of supplying more than 20 high-precision machines worth approximately €5.5 million to Russia in violation of European Union sanctions. Three company employees have been formally charged. Raids were also carried out in Baden-Württemberg and Bulgaria.

According to an investigation by Süddeutsche Zeitung, the company in question is Spinner, based in Sauerlach, a town just outside Munich. Spinner manufactures machine tools at various sites, including near Stuttgart, as well as in Bulgaria and Turkey.

In connection with the investigation, a Spinner machine subject to export restrictions was confiscated in mid-February 2025. Export documents indicated that the machine was supposed to leave Germany in August 2023, traveling through Poland and Belarus on its way to Uzbekistan. Investigators suspect the machine was in fact delivered to a Russian company affiliated with the manufacturer. There is also evidence of additional deliveries through Turkey and China.

The Munich prosecutor’s office cited a detailed report that aired in late April on the TV channel Arte, which traced the export of a Spinner machine to Russia via third countries — allegedly with the use of falsified documents. In the Arte report, one of the company’s three managing directors, Nikolaus Spinner, denied the allegations, claiming the machine had been sold to an Uzbek agricultural equipment manufacturer. However, a manager at the Uzbek company told reporters by phone that no such purchase had taken place.

[…]

0

Production welder/machinist stepping up and in a little over my head

preview

So as the title says, I’ve been a welder for 15 years, and now I’ve been hired into a machinist position, but I’m running the machine shop in this business. I’ve done machining work related to the welding I’ve done, sometimes even working as a machinist when the welding work slows down. My last job was 90% machinist work with 10% welding repair.

Now I’m expected to be a full machinist and run a whole machine section (2 lathes, 2 mills, and an entire wall of disorganized tooling) by myself. To the point where I’m the only guy in the shop that can figure out how to set a power feed on a lathe or mill. It’s a little overwhelming tbh. But I’m struggling through.

Today’s challenge: drill and bore a hole through 10.5 inches of 1018.

What I’ve done:

chucked up the material in the 3 jaw on the lathe

beat around the stock until it was running mostly true (as far as can be read with a dial indicator on mill scale)

Center drilled with 3/8 center drill (only center drill available)

Proceeded to drill through with 9/16 because that’s the only drill we had that was long enough

My problem now:

When the drill popped out the other side, I can see through my spindle it’s maybe 1/8 off center. Definitely wobble as seen from the back of the spindle.

How can I correct the straightness of my hole? The plan was to step up to 1 inch then 2 inch drills to be able to fit in the big boring bar, but i don’t want the bigger drills to follow the pilot off center. Does it matter? Can I just feed the bigger bits slower and the problem will self correct?

Edit: Success! Flipped it around and started a couple inches with a stubby 3/4, then I got an extremely stout 1 3/4 to redrill the hole nice and straight. Once the first couple inches were started it was rigid enough to follow its own hole all the way back through.

So as the title says, I’ve been a welder for 15 years, and now I’ve been hired into a machinist position, but I’m running the machine shop in this business. I’ve done machining work related to the welding I’ve done, sometimes even working as a machinist when the welding work slows down. My last job was 90% machinist work with 10% welding repair.

Now I’m expected to be a full machinist and run a whole machine section (2 lathes, 2 mills, and an entire wall of disorganized tooling) by myself. To the point where I’m the only guy in the shop that can figure out how to set a power feed on a lathe or mill. It’s a little overwhelming tbh. But I’m struggling through.

Today’s challenge: drill and bore a hole through 10.5 inches of 1018.

What I’ve done:

chucked up the material in the 3 jaw on the lathe

beat around the stock until it was running mostly true (as far as can be read with a dial indicator on mill scale)

Center drilled with 3/8 center drill (only center drill available)

Proceeded to drill through with 9/16 because that’s the only drill we had that was long enough

My problem now:

When the drill popped out the other side, I can see through my spindle it’s maybe 1/8 off center. Definitely wobble as seen from the back of the spindle.

How can I correct the straightness of my hole? The plan was to step up to 1 inch then 2 inch drills to be able to fit in the big boring bar, but i don’t want the bigger drills to follow the pilot off center. Does it matter? Can I just feed the bigger bits slower and the problem will self correct?

Edit: Success! Flipped it around and started a couple inches with a stubby 3/4, then I got an extremely stout 1 3/4 to redrill the hole nice and straight. Once the first couple inches were started it was rigid enough to follow its own hole all the way back through.

0

Buddy let me borrow his mill for a project!

preview

So those who know me IRL or cyber stock me. Know that in my free time i do have a very small laser cutting business, i started off with a really crap diode laser and eventually made enough to purchase a full size C02 Laser. Now one of the most important thing that machining has thought me. Is that WORK HOLDING IS BASED. Why indicate a shitty piece of bar stock each time when you can just make a jig/fixture and run thousands with minimal work. So i very much took this to heart and instead of spending 20 minutes to frame a coaster in my laser cutter to make sure it is 100% straight. I took a ratty piece of sheet metal (that i paid WAAAAY to much for $90USD) and made my “ghetto bed”. now it was handcrafted the same way a child makes a macaroni picture. Very imprecise, and not flat at all i tried my best at making it flat but well, im a machinist not a metal worker. which truly shows my 1/1 piccaso’s masterpiece. So i hear you WHERE IS THIS GOING!! this “ghetto bed” worked very well for small stuff, when family and friends would order something i would quickly throw in my jig load up my file and BAM its ready to go. This bed was purely a proof of concept, from the post i saw on light-burns forum of a guy doing something similar with sheet metal. So fast foward 3 years later and i bought plate 3/4 plate stock (which i paid out the ass for) order it to size and draw up a CAD model. a few thing i learned from the original “ghetto bed” was that the exhaust is underneath the bed and needed some way to quickly slurp up the smoke, for this i have a snorkel i am 3d printing and running downward (still work in progress as we speak) and secondly and most importantly! I wanted threading, i originally drilled 7/16 holes to which i just vaguely threaded bolts and nuts through. But now i have 1/4-20 spaces 1.30 inches across the bed, which will make setting up fixtures more solid and repeatable unlike the original bed. i did go with 1/4-20 for a few reasons, first off its standardized and very cheap for bolts, second and most importantly its a small hole. Which then allows me to drill and re-tap if i strip a thread and it also gives me alot of mounting holes. However having tons of holes were also a nightmare to hand tap and debur the backside.

The keen eyed among you may notice slots on the edges of the bed, i decided to go with slots purely because the original mounting holes are not concentric or symmetrical. So F it slots!

im very happy with the bed, i plan to paint it black to make it not reflective and have played around with the idea of open sourcing/selling bed like this, if people are intreasted of course!

So those who know me IRL or cyber stock me. Know that in my free time i do have a very small laser cutting business, i started off with a really crap diode laser and eventually made enough to purchase a full size C02 Laser. Now one of the most important thing that machining has thought me. Is that WORK HOLDING IS BASED. Why indicate a shitty piece of bar stock each time when you can just make a jig/fixture and run thousands with minimal work. So i very much took this to heart and instead of spending 20 minutes to frame a coaster in my laser cutter to make sure it is 100% straight. I took a ratty piece of sheet metal (that i paid WAAAAY to much for $90USD) and made my “ghetto bed”. now it was handcrafted the same way a child makes a macaroni picture. Very imprecise, and not flat at all i tried my best at making it flat but well, im a machinist not a metal worker. which truly shows my 1/1 piccaso’s masterpiece. So i hear you WHERE IS THIS GOING!! this “ghetto bed” worked very well for small stuff, when family and friends would order something i would quickly throw in my jig load up my file and BAM its ready to go. This bed was purely a proof of concept, from the post i saw on light-burns forum of a guy doing something similar with sheet metal. So fast foward 3 years later and i bought plate 3/4 plate stock (which i paid out the ass for) order it to size and draw up a CAD model. a few thing i learned from the original “ghetto bed” was that the exhaust is underneath the bed and needed some way to quickly slurp up the smoke, for this i have a snorkel i am 3d printing and running downward (still work in progress as we speak) and secondly and most importantly! I wanted threading, i originally drilled 7/16 holes to which i just vaguely threaded bolts and nuts through. But now i have 1/4-20 spaces 1.30 inches across the bed, which will make setting up fixtures more solid and repeatable unlike the original bed. i did go with 1/4-20 for a few reasons, first off its standardized and very cheap for bolts, second and most importantly its a small hole. Which then allows me to drill and re-tap if i strip a thread and it also gives me alot of mounting holes. However having tons of holes were also a nightmare to hand tap and debur the backside.

The keen eyed among you may notice slots on the edges of the bed, i decided to go with slots purely because the original mounting holes are not concentric or symmetrical. So F it slots!

im very happy with the bed, i plan to paint it black to make it not reflective and have played around with the idea of open sourcing/selling bed like this, if people are intreasted of course!

0

HAAS cuts production due to tariffs

IndustryWeek So That Happened: Haas Cuts California Manufacturing Because of Tariffs www.industryweek.com
preview

Haas Reduces Production, Slashes Overtime in California

With the vast majority of global machine tools coming out of Europe and Asia, California-based Haas Automation might sound like it’s in a perfect position to benefit from tariffs placed on imports that President Donald Trump says will kickstart American manufacturing.

However, any longer-term reshoring is way off in the distance. Instead, Haas is facing an immediate pullback in production from its manufacturing customers as they weigh increases in raw materials and components prices.

“In recent days, we’ve seen a dramatic decrease in demand for our machine tools from both domestic and foreign customers,” Haas automations official said. “Out of caution, we have reduced production and eliminated overtime at our sole manufacturing plant in Oxnard, California, where we employ 1,700 workers and have been in operation since 1983. We have also halted hiring and put new employment requisitions on hold.”

Because reshoring will require new equipment, Haas officials said they’re worried that the administration could slash tariffs on machines from Taiwan (companies such as YCM and Hartford), Japan (Okuma, Makino) and Korea (DN Solutions, Hwacheon) to avoid making manufacturing investments in the U.S. more expensive.

Worse, Haas imports some of the materials and components it uses in its machine tools, so tariff breaks for Asian machine tool makers could give them a major cost advantage over American-produced machines.

“Without a corresponding reduction in tariff rates for imported raw materials and components into the U.S., such a scenario would be catastrophic to the $5 billion U.S. machine tool industry, which is a key component of U.S. national security,” Haas officials said.

—Robert Schoenberger

industryweek.com/…/so-that-happened-haas-cuts-cal…

Haas Reduces Production, Slashes Overtime in California

With the vast majority of global machine tools coming out of Europe and Asia, California-based Haas Automation might sound like it’s in a perfect position to benefit from tariffs placed on imports that President Donald Trump says will kickstart American manufacturing.

However, any longer-term reshoring is way off in the distance. Instead, Haas is facing an immediate pullback in production from its manufacturing customers as they weigh increases in raw materials and components prices.

“In recent days, we’ve seen a dramatic decrease in demand for our machine tools from both domestic and foreign customers,” Haas automations official said. “Out of caution, we have reduced production and eliminated overtime at our sole manufacturing plant in Oxnard, California, where we employ 1,700 workers and have been in operation since 1983. We have also halted hiring and put new employment requisitions on hold.”

Because reshoring will require new equipment, Haas officials said they’re worried that the administration could slash tariffs on machines from Taiwan (companies such as YCM and Hartford), Japan (Okuma, Makino) and Korea (DN Solutions, Hwacheon) to avoid making manufacturing investments in the U.S. more expensive.

Worse, Haas imports some of the materials and components it uses in its machine tools, so tariff breaks for Asian machine tool makers could give them a major cost advantage over American-produced machines.

“Without a corresponding reduction in tariff rates for imported raw materials and components into the U.S., such a scenario would be catastrophic to the $5 billion U.S. machine tool industry, which is a key component of U.S. national security,” Haas officials said.

—Robert Schoenberger

industryweek.com/…/so-that-happened-haas-cuts-cal…

0

Precision spindle metrology part 1

play · youtube.com
YouTube PRECISION SPINDLE METROLOGY Pt. 1: Fundamental Concepts youtu.be
preview

This is a really good 3 part series on measuring the error motion of a precision spindle that I found really interesting and wanted to share.

This is a really good 3 part series on measuring the error motion of a precision spindle that I found really interesting and wanted to share.

0

Constructing A Byzantine Sundial-Calendar - Part 6 (Etching & Waxing The Dials)

play · youtube.com
YouTube Constructing A Byzantine Sundial-Calendar - Part 6 (Etching & Waxing The Dials) www.youtube.com
preview

Consider watching this video with FreeTube, a nifty open-source program that lets you watch YouTube videos without Google spying on your viewing habits!

Combined with Libredirect, which automatically opens youtube links in Freetube, it becomes really slick and effortless to use.

Consider watching this video with FreeTube, a nifty open-source program that lets you watch YouTube videos without Google spying on your viewing habits!

Combined with Libredirect, which automatically opens youtube links in Freetube, it becomes really slick and effortless to use.

0

Constructing A Byzantine Sundial-Calendar - Part 5 (Making The Supporting Bridges)

play · youtube.com
YouTube Constructing A Byzantine Sundial-Calendar - Part 5 (Making The Supporting Bridges) www.youtube.com
preview

Consider watching this video with FreeTube, a nifty open-source program that lets you watch YouTube videos without Google spying on your viewing habits!

Combined with Libredirect, which automatically opens youtube links in Freetube, it becomes really slick and effortless to use.

Consider watching this video with FreeTube, a nifty open-source program that lets you watch YouTube videos without Google spying on your viewing habits!

Combined with Libredirect, which automatically opens youtube links in Freetube, it becomes really slick and effortless to use.

0

Constructing A Byzantine Sundial-Calendar - Part 4 (Depthing & Planting The Gear Train)

play · youtube.com
YouTube Constructing A Byzantine Sundial-Calendar - Part 4 (Depthing & Planting The Gear Train) www.youtube.com
preview

With Google’s assault on Invidious leaving it inoperable, consider watching this video with FreeTube, a nifty open source program that lets you watch youtube videos privately!

With Google’s assault on Invidious leaving it inoperable, consider watching this video with FreeTube, a nifty open source program that lets you watch youtube videos privately!

0

This button makes thread cutting too easy | Not An Engineer

YouTube How I gave my lathe a "nut" button, and why I'll never look back www.youtube.com
preview

With Google’s assault on Invidious leaving it inoperable, consider watching this video with FreeTube, a nifty open source program that lets you watch youtube videos privately!

With Google’s assault on Invidious leaving it inoperable, consider watching this video with FreeTube, a nifty open source program that lets you watch youtube videos privately!

0

Saying goodbye tomorrow to a couple of guys I knew.

preview

Xpost from casual conversations. Delete if it doesn’t fit.

In the final stages of moving from the deep south to a northern state.

I used to run a shop under a corporation. Long story, but I integrated the shop, and built something beautiful. I had to use a temp service to do a lot of my hiring, I hired lots of black folks because they were undervalued and I could give them a good environment and pay. Was just starting to hire women. COVID and Qanon blew it the fuck up.

Tomorrow I’ll be having lunch with two of my former crew. One of them is the only man I’ve ever called brother. He was my neighbor and best friend for years. I would have trusted him to help me hide a body. The other feller was a kind and gentle guy, had a bad divorce but was a teddy bear, was on the road back up.

They both went down the rabbit hole real bad.

I miss who they were and the shop we had. It was fucking jazz. I protected all of them from corporate. We made shit happen. I fought to get them more money and got fucked over myself.

I’ve lost my parents, my grandfather, my aunts and uncles and cousins to the insanity. Thank jeebus my grandmothers and one grandfather are dead.

Tomorrow I’m going to hug my brother and tell him goodbye. He isn’t really my brother anymore. I don’t trust him. I love him. He’s not the man I knew.

It hurts a lot. It broke my heart.

Xpost from casual conversations. Delete if it doesn’t fit.

In the final stages of moving from the deep south to a northern state.

I used to run a shop under a corporation. Long story, but I integrated the shop, and built something beautiful. I had to use a temp service to do a lot of my hiring, I hired lots of black folks because they were undervalued and I could give them a good environment and pay. Was just starting to hire women. COVID and Qanon blew it the fuck up.

Tomorrow I’ll be having lunch with two of my former crew. One of them is the only man I’ve ever called brother. He was my neighbor and best friend for years. I would have trusted him to help me hide a body. The other feller was a kind and gentle guy, had a bad divorce but was a teddy bear, was on the road back up.

They both went down the rabbit hole real bad.

I miss who they were and the shop we had. It was fucking jazz. I protected all of them from corporate. We made shit happen. I fought to get them more money and got fucked over myself.

I’ve lost my parents, my grandfather, my aunts and uncles and cousins to the insanity. Thank jeebus my grandmothers and one grandfather are dead.

Tomorrow I’m going to hug my brother and tell him goodbye. He isn’t really my brother anymore. I don’t trust him. I love him. He’s not the man I knew.

It hurts a lot. It broke my heart.

0

Stainless Steel Spikes (electrodes)

preview

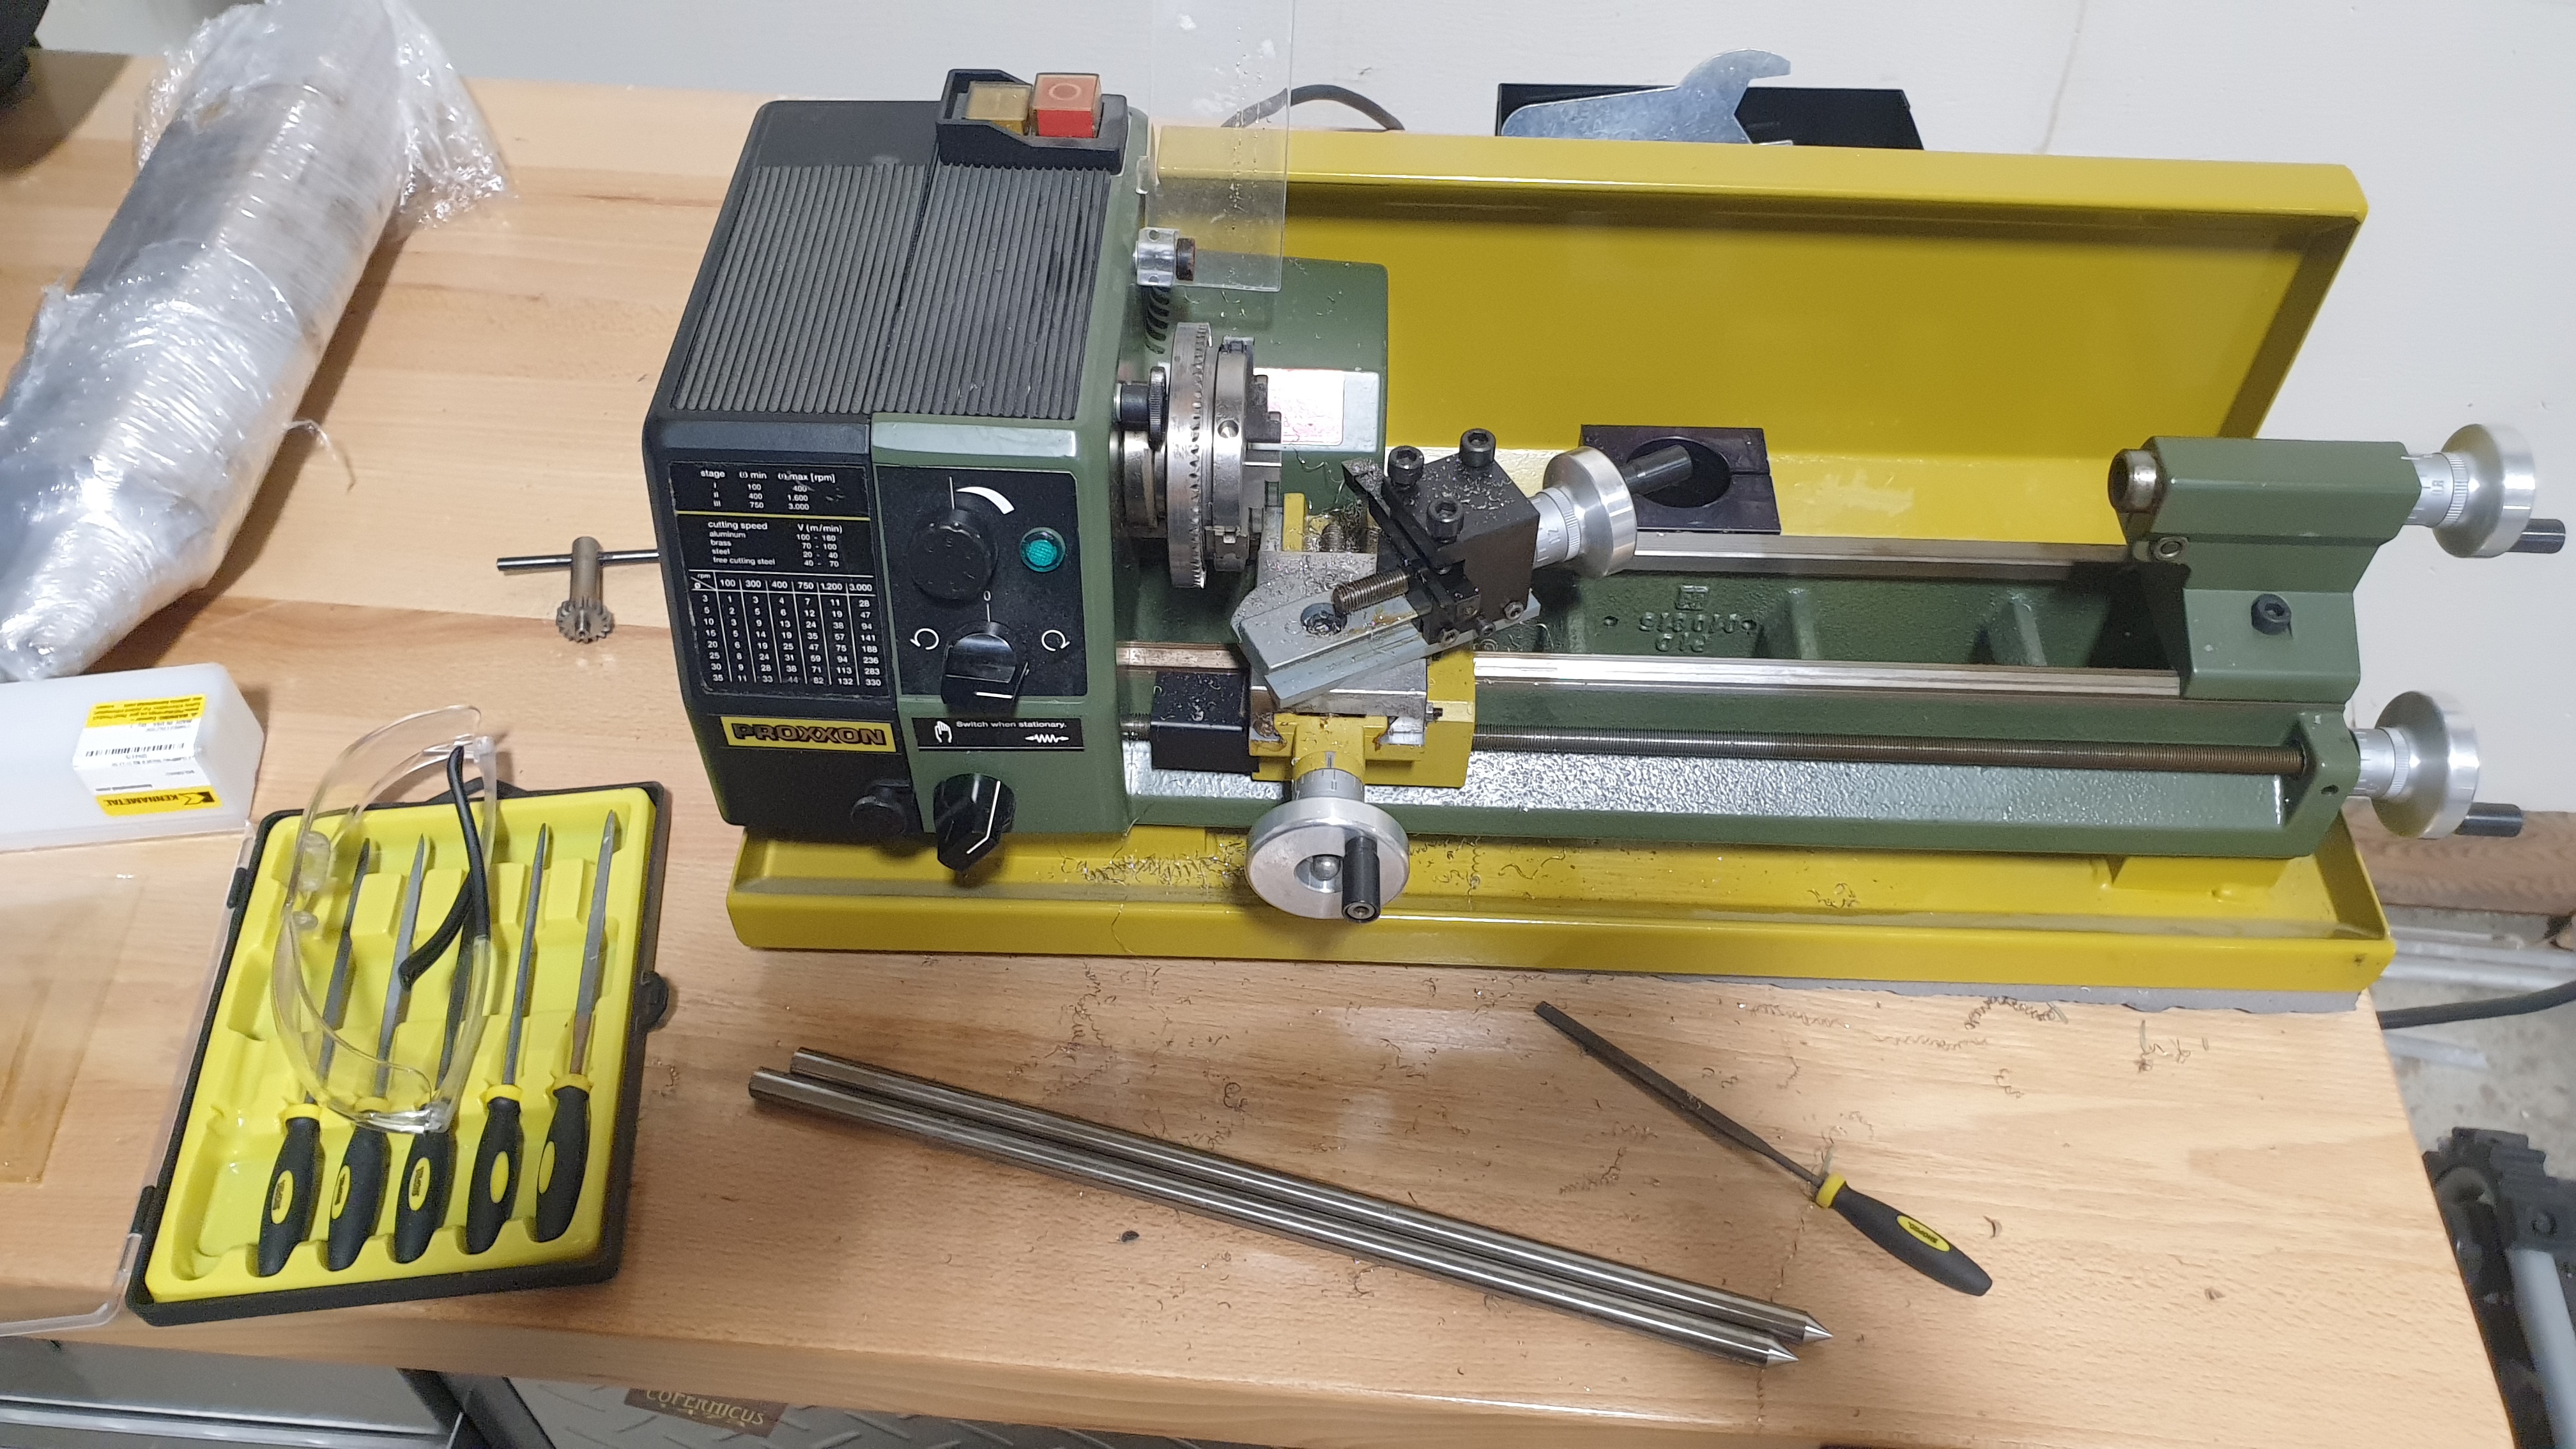
Hey folks, pardon the rookie question. We need to build a few hundred of these per year, so I thought I’d tool up, and wanted to figure out how to do this “cheaply”.

Parameters. Stainless steel rods, with one end sharpened to a point, and the other end deburred. Typically 30cm long with no real tolerance issues, and no real parameters on the point other than “if you hit it with a hammer, you should be able to drive them into the earth.” Typically made of 3/8" or 1/2" stainless.

My main problem is: stainless is fucking hard and destroys my bench grinder when grinding tips onto it. Is there a better grinder I could be using? Or perhaps I should be cutting these on a small lathe?

Also, when I buy stainless stock, I usually have the metal wholesaler cut them to length for us, but they charge quite a bit. The stainless destroys my bandsaw blades, so perhaps there is a better option? Is there a mitre saw blade that is rated for stainless? Or should I also be using a parting tool on a lathe here?

Thoughts are appreciated. Such a simple thing, but stainless so…

Hey folks, pardon the rookie question. We need to build a few hundred of these per year, so I thought I’d tool up, and wanted to figure out how to do this “cheaply”.

Parameters. Stainless steel rods, with one end sharpened to a point, and the other end deburred. Typically 30cm long with no real tolerance issues, and no real parameters on the point other than “if you hit it with a hammer, you should be able to drive them into the earth.” Typically made of 3/8" or 1/2" stainless.

My main problem is: stainless is fucking hard and destroys my bench grinder when grinding tips onto it. Is there a better grinder I could be using? Or perhaps I should be cutting these on a small lathe?

Also, when I buy stainless stock, I usually have the metal wholesaler cut them to length for us, but they charge quite a bit. The stainless destroys my bandsaw blades, so perhaps there is a better option? Is there a mitre saw blade that is rated for stainless? Or should I also be using a parting tool on a lathe here?

Thoughts are appreciated. Such a simple thing, but stainless so…